One-Piece Flow: Intelligent Stacking Forklift for a Tire Plant Warehouse

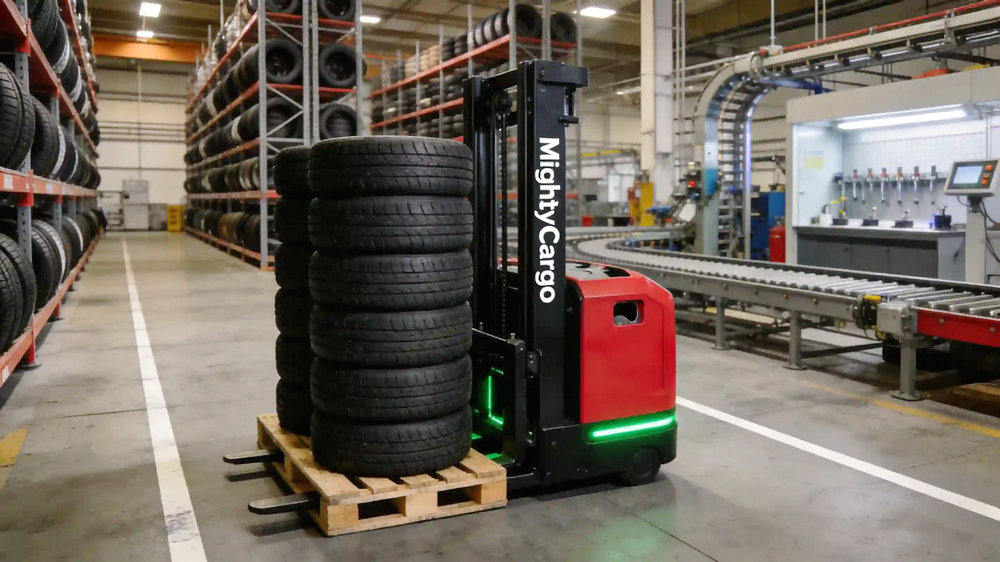
MightyCargo intelligent stacking forklifts linked to roller conveyors and WMS automate tire line-off, high-bay putaway and order picking — line-to-storage cycle down from 12 to 4 minutes per pallet.

Tire & Auto Parts Logistics — case study image

Tire Manufacturing & Auto Parts Logistics

Project overview

The client is a leading automobile tire manufacturer with tire vulcanization and molding lines and a supporting stereoscopic finished-goods warehouse. The workshop produces more than 10,000 passenger tires a day, stored as whole pallet stacks before shipment to vehicle OEM plants.

The original warehouse relied on manual powered stackers, suffering from slow high-rack access, high labor cost, tire stack damage and weak line-to-warehouse handoff. MightyCargo intelligent stacking forklifts were linked with the production line's roller conveyors and the WMS, automating the entire flow from tire line-off, putaway and order picking — a benchmark of intelligent tire warehousing.

Equipment deployed: Intelligent stacking forklifts + roller conveyors + WMS

What the customer faced

  • Low high-rack efficiency — manual stackers work slowly at height and underutilize upper rack levels.
  • High labor cost and damage — human handling damages tire stacks; handoffs lag between line and warehouse.
  • Discontinuous flow — night shifts wait for drivers instead of matching the plant's 24-hour output.

How MightyCargo answered

Line-end pickup — seamless handoff, gentle handling

After vulcanization and QC, tires are collected on roller conveyors and stacked on standard wooden pallets awaiting storage. The WMS synchronizes line completion data in real time and issues pickup orders to the MightyCargo intelligent forklift, which travels autonomously to the line outlet, aligns precisely with the conveyor and forks the full pallet smoothly. Because passenger tires stack in multiple layers with round, easily scuffed cargo, the forklift's high-precision hydraulic lifting and anti-sway fork control eliminate scraping and deformation — tire damage is down 90% versus manual operation. With three-shift continuous production, the intelligent forklift cycles around the clock with no shift-change waiting, perfectly matching uninterrupted line output and ending the night-time wait for forklift drivers.

High-bay storage — dense racks, fully used

The finished tire warehouse uses multi-level heavy racks with narrow aisles and significant height. The compact MightyCargo body navigates the narrow aisles and, with multi-stage mast lifting, puts pallets several meters up — activating upper rack levels that used to sit idle and lifting overall warehouse capacity utilization 35%. On OEM order outbound instructions, the forklift autonomously picks tire pallets from the correct cells and transfers them to the outbound sorting area; the system records outbound model and quantity and updates inventory automatically — no manual searching or counting. Tires are stored by spec (size, vehicle model) with system-dispatched, category-based putaway, so cross-model misplacement drops sharply and picking errors approach zero.

Measured impact

6 → 1

certified operators

The tire storage zone's 6 licensed forklift operators were reduced to 1 field O&M staff, cutting annual labor cost; automated gentle handling also lowers damage loss each year.

12 → 4 min

per pallet, line to storage

Single-pallet flow from line-off to warehouse fell from 12 to 4 minutes; daily warehouse throughput rose 40%, matching the plant's capacity expansion.

0

materials on record

Routine operations data uploads to the plant's MES/WMS in real time — inbound, outbound and inventory are traceable across the whole chain, enabling refined inventory control and reducing dead stock and tied-up capital.

Industry value

Extending the value

This MightyCargo intelligent tire-warehouse solution extends to commercial-vehicle tire plants and tire distributor stereoscopic warehouses, and fits rubber spare parts, wheel hubs and other round or stacked auto-parts goods — the preferred blueprint for intelligent automotive-parts warehousing.

Keep reading

Electric Power Equipment Manufacturing — case study

Electric Power & Equipment Manufacturing

Electric Power Equipment Manufacturing

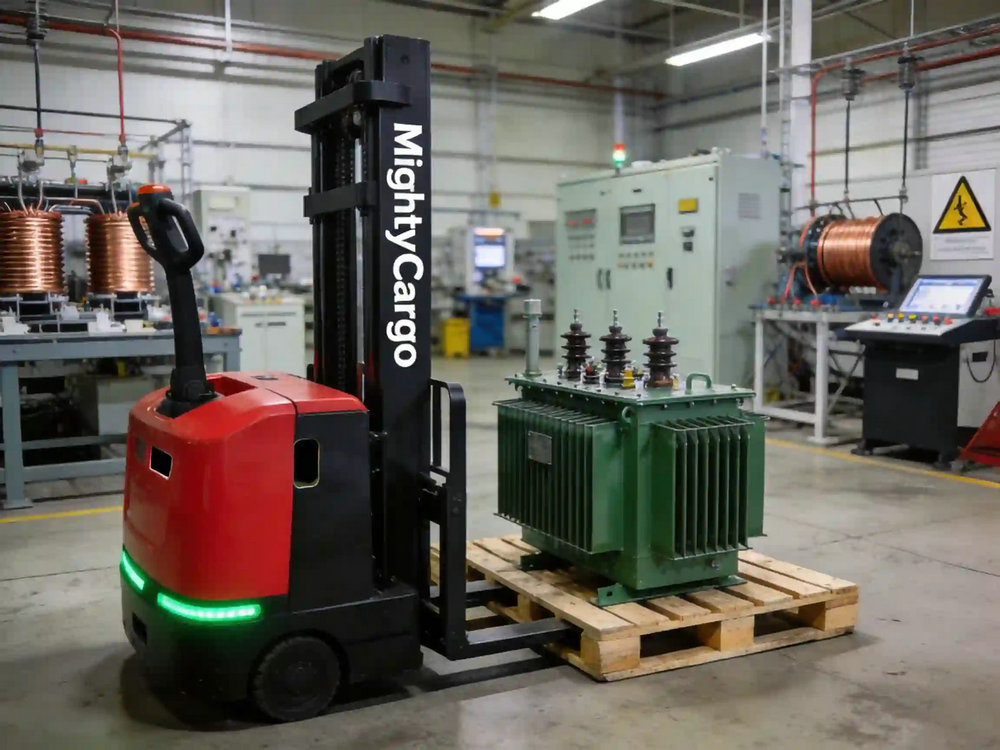
A large power transformer manufacturer replaced struggling manual handling with a compact fork-type AMR that shuttles 0.8–3 t transformer units through 1.6 m aisles — transfer time cut from 20 to 3 minutes per unit.

Read the case
Hazardous Chemical Industry — case study

Chemicals & Hazardous Goods

Hazardous Chemical Industry

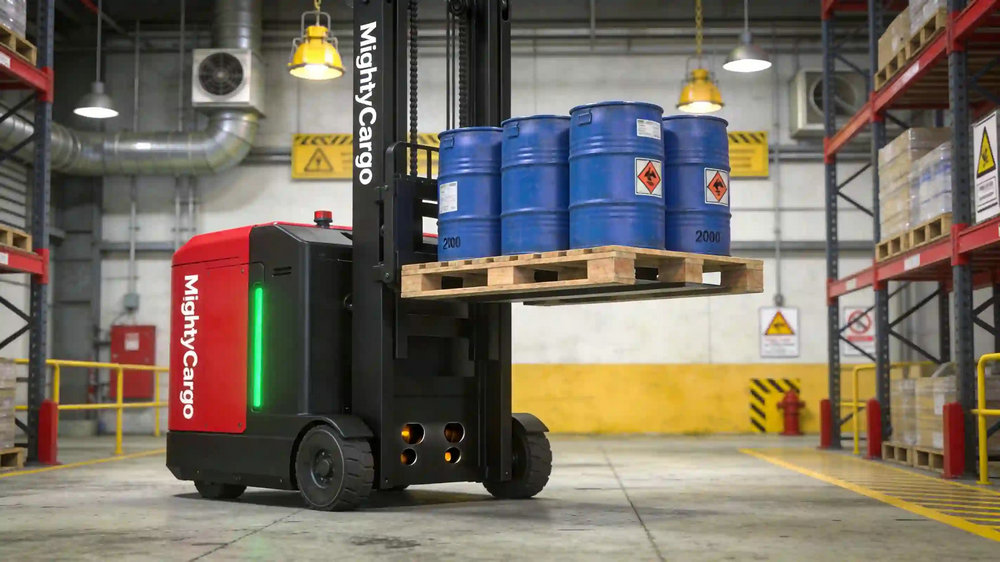
Explosion-proof electric stackers, automated AGV forklifts and counterbalance trucks together digitize raw-material intake, process feeding and finished-goods storage at a fine chemical plant — drum handling accidents down 95%.

Read the case
Steel & Metallurgy — case study

Steel & Metallurgy

Steel & Metallurgy

In the extreme environment of a steel plant — radiant heat, dust, heavy impact and 7×24 rhythm — heavy forklifts, reach trucks and a new generation of AGVs form a heat-resistant, dust-proof, high-precision collaborative system.

Read the case

Ready to upgrade your material handling?

Tell us about your warehouse, factory or port challenge — our engineers will recommend the right MightyCargo solution for your loads, aisles and duty cycles.

↑