Safe by Design: Explosion-Proof Handling for a Fine Chemical Plant

Explosion-proof electric stackers, automated AGV forklifts and counterbalance trucks together digitize raw-material intake, process feeding and finished-goods storage at a fine chemical plant — drum handling accidents down 95%.

Hazardous Chemical Industry — case study image

Chemicals & Hazardous Goods

Project overview

The client is a large fine chemical manufacturer producing organic solvents, chemical powders and liquid intermediates. The site is divided into a production/process zone, a hazardous raw-material stereoscopic warehouse and a finished-goods warehouse, handling 200 L drums of hazardous liquids, IBC totes of solvents and bagged chemical powders.

Manual handling of hazardous materials carried three major risks: tipping and leakage of hazardous drums, mis-storage and mixing across chemical categories, and difficulty staffing hot or night-shift operations — plus handling damage to raw materials. MightyCargo deployed a combined solution of counterbalance forklifts, explosion-proof electric stackers and fully automatic AGV forklifts, covering raw-material intake, process feeding and finished-goods putaway for a safer, digital, more efficient chemical warehouse.

Equipment deployed: Counterbalance forklifts + explosion-proof electric stackers + fully automatic AGV forklifts

What the customer faced

  • Hazardous-drum handling — manual transfer risks tipping, leakage and ignition of flammable solvents.
  • Multi-category storage — high risk of mis-storage or mixing different chemical types in the warehouse.
  • Labor constraints — high-temperature and night-shift work is hard to staff; manual forking damages raw materials.

How MightyCargo answered

Scene 1 — process feeding: explosion-proof counterbalance electric forklift

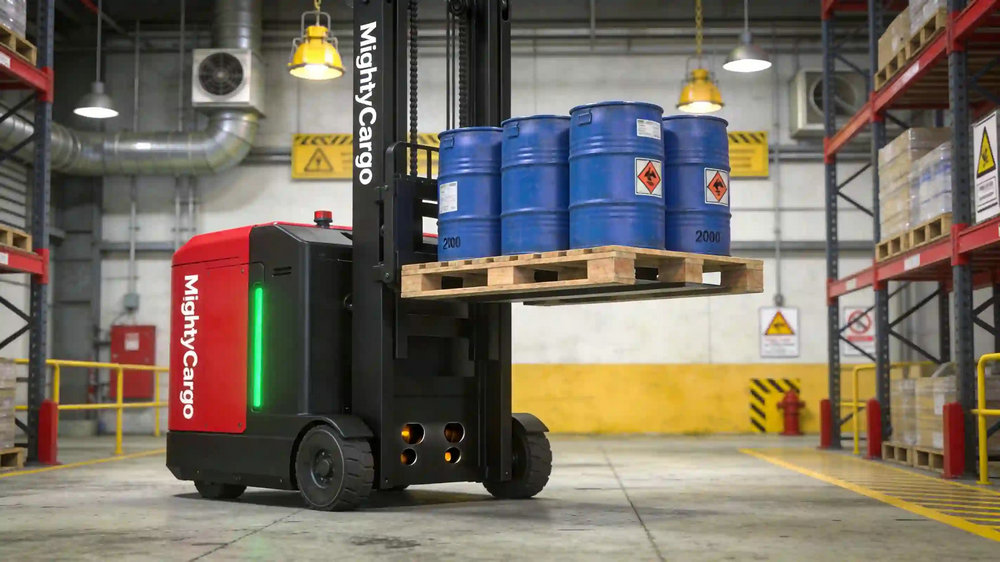
Reactor support tanks need a constant supply of drummed organic solvents; 200 L chemical drums are stored as whole pallets and transferred from the raw-material yard to process feed points. The MightyCargo explosion-proof counterbalance electric forklift features explosion-proof electronic control and a flame-retardant hydraulic system for flammable atmospheres: forks center precisely on standard chemical drum pallets, and a cushioned mast prevents drum cracking and liquid leakage from travel bumps — eliminating solvent-leak fire risk. For outdoor, all-weather duty, sealed motors and wear-resistant tires suit rough yard surfaces, moving bagged powders (calcium carbonate, additives, etc.) whole-pallet from the yard to the dosing workshop — replacing aging fuel trucks and removing exhaust corrosion and explosion-compliance concerns.

Scene 2 — high-bay hazardous storage: explosion-proof electric stacker

The finished hazardous warehouse uses multi-level heavy racks with IBC totes and drummed chemicals stored by zone at 6 m heights in narrow aisles. The MightyCargo walkie explosion-proof stacker is the zone's main equipment: a compact body works narrow aisles and a multi-stage lift mast puts totes and drums at high levels, maximizing stereoscopic storage; solvents are segregated by type (alcohols, esters) to eliminate chemical-mixing reaction hazards. Explosion-proof electricals and spark-proof wheels meet the fire code for Class A hazardous warehouses — human-supervised duty that removes the risk of sparks igniting volatile vapors.

Scene 3 — clean raw-material warehouse: automated AGV cluster

A newly built clean intermediate-materials warehouse stores food-grade IBC totes and must tightly control dust and personnel entry. Multiple MightyCargo underride-lifting AGVs plus stacking AGVs are integrated with the WMS: raw materials are palletized at unloading, AGVs pick them up automatically, follow mapped routes into the rack area and complete autonomous high putaway; on production feeding orders, the system picks the matching totes and transfers them to the outbound dock — with no personnel entering the clean zone. Multi-vehicle zone dispatch plans paths automatically, avoids congestion and collisions, and supports 24-hour continuous feeding with unattended night shifts — solving the chemical industry's night-shift staffing problem.

Measured impact

−95%

drum handling accidents

Explosion-proof equipment plus automation cut chemical drum tipping/leakage accidents by 95%; mis-storage and mixing hazards are basically eliminated, and the site passed the regulatory hazardous-warehouse compliance review.

12 → 2

staff on site

The original 12 forklift drivers across warehouse and workshop were reduced to 2 equipment O&M staff — saving over 300,000 RMB a year in labor.

+180k RMB/yr

materials recovered

Automated stable picking cuts drum damage, recovering about 180,000 RMB a year of raw-material losses.

15 → 5 min

per pallet in

Manual single-pallet inbound took 15 minutes; automation shortens it to 5 minutes, lifting daily warehouse throughput 50% — matching the plant's 120,000 t/yr capacity expansion.

Industry value

Extending the value

The explosion-proof forklift plus intelligent AGV package can be replicated widely in petrochemical, coatings, pharmaceutical intermediates and agrochemical manufacturing — with models selected by Class A/B/C hazardous-warehouse ratings. It is the standardized blueprint for chemical warehouse intelligence and safety upgrades.

Keep reading

Electric Power Equipment Manufacturing — case study

Electric Power & Equipment Manufacturing

Electric Power Equipment Manufacturing

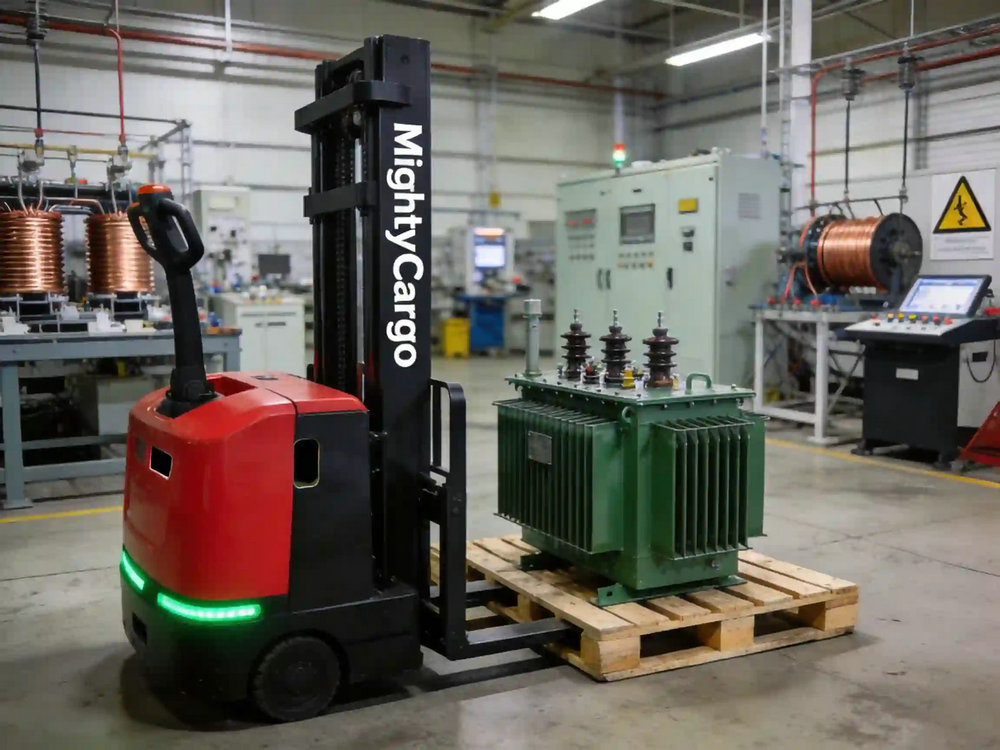
A large power transformer manufacturer replaced struggling manual handling with a compact fork-type AMR that shuttles 0.8–3 t transformer units through 1.6 m aisles — transfer time cut from 20 to 3 minutes per unit.

Read the case
Tire & Auto Parts Logistics — case study

Tire Manufacturing & Auto Parts Logistics

Tire & Auto Parts Logistics

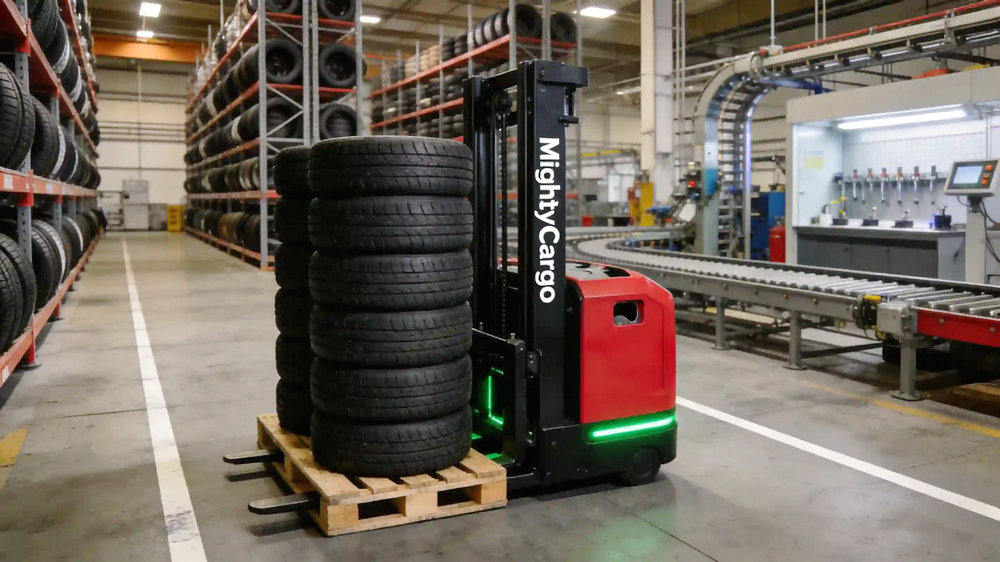
MightyCargo intelligent stacking forklifts linked to roller conveyors and WMS automate tire line-off, high-bay putaway and order picking — line-to-storage cycle down from 12 to 4 minutes per pallet.

Read the case
Steel & Metallurgy — case study

Steel & Metallurgy

Steel & Metallurgy

In the extreme environment of a steel plant — radiant heat, dust, heavy impact and 7×24 rhythm — heavy forklifts, reach trucks and a new generation of AGVs form a heat-resistant, dust-proof, high-precision collaborative system.

Read the case

Ready to upgrade your material handling?

Tell us about your warehouse, factory or port challenge — our engineers will recommend the right MightyCargo solution for your loads, aisles and duty cycles.

↑